
- Sourcing CNC machining? The test is not the tolerance printed on a brochure — it is whether the shop can hand you a CMM report for the exact feature you are buying, with the band, the sample size and the study window all named.
- What CNC machining is: a subtractive process — a cutter removes material from a workpiece along a programmed toolpath until the geometry, tolerance and surface finish on the drawing exist.
- A 6,800 m² floor of named equipment — Mazak, Brother, Tsugami, Star and Citizen machines (3-axis 50+, 4-axis 20+, 5-axis 20+, 25+ lathes, 7+ grinders, 20+ inspection instruments).
- Measured, not claimed: ±0.003 mm, turning ±0.002 mm, grinding ±0.002 mm, verified on Hexagon CMMs. Per-characteristic capability is Ppk ≥ 1.67 initial and Cpk ≥ 1.33 production (≥ 1.33 general). Reports name the feature, band, sample size, sigma method and window.
- Certified under ISO 9001:2015, IATF 16949:2016 (design excluded) and ISO 14001:2015 — Dongguan Zhuohang Ltd is the invoicing entity behind them.
- Order terms: MOQ 1 piece, lead times of roughly 3 / 7 / 30 days depending on complexity.
What is a CNC machining shop?
A CNC machining shop is a business whose floor is machines, not a desk that forwards drawings to someone else. This one runs 100+ CNC machines in Dongguan under ISO 9001:2015 and IATF 16949:2016, holding ±0.003 mm on milling and ±0.002 mm on turning, verified on Hexagon CMMs. The difference between a real shop and a trading desk shows up in the machine list and the floor video.
CNC machining is the subtractive manufacturing of parts on computer-numerically-controlled milling, turning, and grinding equipment. A cutter removes material from a workpiece along a programmed toolpath to produce a part that meets a drawing-defined geometry, tolerance, and surface finish. "CNC" means the tool path is numerically controlled rather than hand-operated.
The rest of this guide turns that definition into a buyer's checklist for this shop — what to verify before you commit, and how the numbers on the drawing actually reach the part.
The discipline separates into milling (the cutter rotates and the workpiece is fed; prismatic geometry), turning (the workpiece rotates and the tool is fed; rotational geometry), and precision grinding / wire EDM (the tightest tolerances on critical features). A plant that produces CNC machined parts end-to-end runs all three.
The output of CNC machining is a part that meets the drawing — geometry, tolerance, surface finish, and material certificate — and is documented to a quality plan (FAI for general work, PPAP for automotive-bound parts, IMDS for material data). That is the answer to "what is CNC machining": a numerically-controlled subtractive process that produces a part to a drawing, with the quality documentation that lets the part enter an assembly.
- 100+ machines, named by brand (Mazak, Brother, Citizen, Star, Tsugami) - not a stock photo. ±0.003 mm CNC milling, ±0.002 mm CNC turning; ±0.002 mm grinding.
- 6,800 m² facility, 100+ staff, founded 2005.
- Measurement on Hexagon CMMs, KEYENCE, XRF, micro-Vickers, Fischer, salt-spray, tensile.
- Ppk ≥ 1.67 initial on critical, ≥ 1.33 on general characteristics.
- MOQ 1 piece; lead time 3 / 7 / 30 days.
How do you tell a real machine shop from a trading desk?

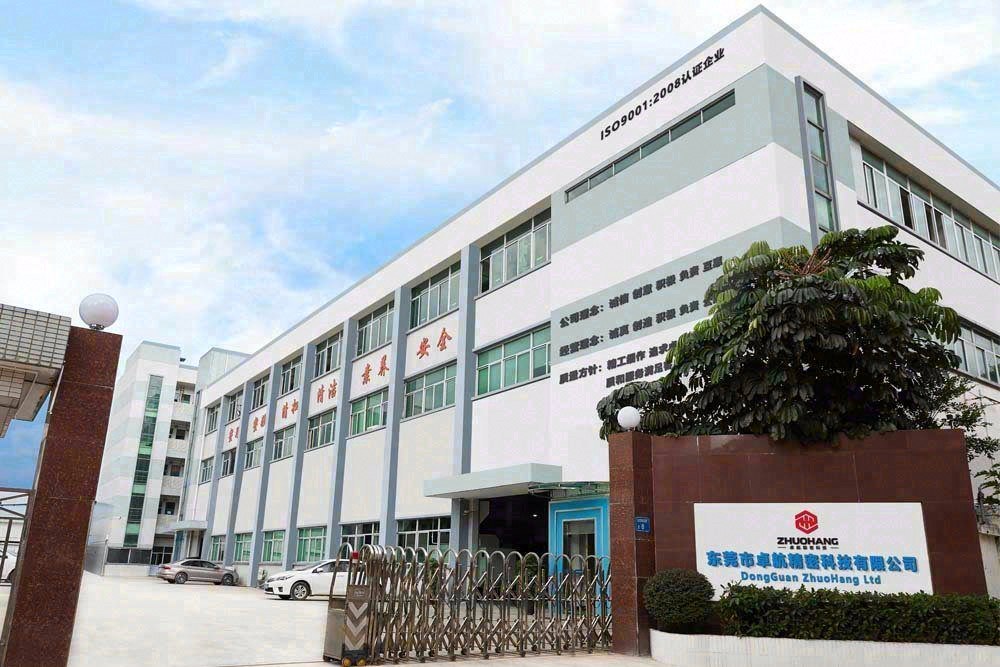
The first risk in sourcing CNC parts is not tolerance, it is whether the shop exists as described. A trading desk will show you a brochure and a logo; a manufacturer will show you the machine list with model names and a count you can reconcile against the building. We are Dongguan Zhuohang Ltd, trading as Zhuohang Precision Machining Factory and Zhuohang Precision Machining Factory, business registration 91441900MA4UWT6X39, founded in 2005 in Hengli Town, Dongguan. Ask for the registration number up front. A certificate or a capability claim tied to a name you cannot verify is worth less than the paper it is printed on.
Capacity is the sum of what is physically on the floor, not what a sales deck implies. Before you send a drawing, you should be able to name the brands running your part, the count of each, and the measurement equipment that proves the result. If a supplier answers those three questions with hesitation, that hesitation is the answer.
The reason this matters is structural, not cosmetic. A trading desk buys from a network of shops it does not operate, so it cannot control a setup, a corrective action, or a certificate scope. When a part fails, you deal with an intermediary who has to relay your problem to a shop you never vetted. A manufacturer answers directly, because the machine, the operator, and the quality system all sit under the same roof. That difference shows up first in paperwork — a manufacturer sends certificate numbers, machine counts, and a legal entity in writing, without being asked twice.
There is a simple test that cuts through most of the noise: ask the supplier to state its legal entity, registration number, and certificate numbers in the first reply. A manufacturer writes them down because they are facts it owns. An intermediary changes the subject to samples and timelines, because those are the only things it can actually show. The entity behind the brand is the anchor every other claim hangs from, and if it is missing, nothing else is load-bearing.
What should the machine list actually tell you?
A credible shop names its machines. We run more than 80 machines, including Mazak five-axis and turning centers, Brother high-speed machining centers, Citizen and Star Swiss-type lathes, and Tsugami precision turning and mill-turn units. Naming brands matters because each carries a documented accuracy class and a service history you can reason about. A Swiss-type Citizen or Star holds diameter and length consistency across long runs that a manual lathe cannot, and a Brother center holds tight positional repeatability on high-mix work.
When you receive a machine list, read it as a capability map. Count the spindle hours available, the balance between 3-axis, 4-axis, 5-axis, and turning, and whether mill-turn is present for one-setup work. That map predicts whether your job shares the line with a thousand others or gets dedicated capacity.
A useful machine list also separates what a shop owns from what it subcontracts. If anodizing, heat treatment, or grinding leaves the building, the list should say so and name the partner. The partner is now part of your supply chain and your risk, and a shop that hides that is hiding a cost and a control gap, not a convenience.
Three patterns on a machine list tell you more than the totals do. First, a list of brand names with no model numbers is marketing; a real list names models, because accuracy class lives in the model. Second, a list that counts "CNC machines" without splitting 3-axis, 4-axis, 5-axis, and turning hides the mix your part actually needs. Third, a list with no inspection equipment next to it tells you the shop machines and someone else measures, which is where the tolerance claim quietly ends. Read for the split, not the headline.
- Brand names without model numbers are marketing, not capability.
- A single "CNC machines" count hides the axis mix your part needs.
- No inspection equipment on the list means someone else holds the tolerance.
Why does machine count matter more than a photo?
A single photo of a Mazak proves one machine. More than 80 machines across brands means a load-balanced line: when one machine is tied up in a long setup, another runs your urgent lot. It also means spare capacity for a prototype insert without bumping a production job. We run more than 80 machines, so a single order rarely waits on a single asset.
Count also predicts delivery honesty. A two-machine shop that quotes five simultaneous jobs has to either delay some of them or quietly subcontract. A floor with 50+ three-axis centers, 20+ four-axis, 20+ five-axis, 25+ lathes, and 7+ grinders can absorb a spike without lying about it. When you read a machine list, you are really reading the shop's ability to keep a promise without borrowing someone else's capacity.
This is the difference between a shop that quotes what it can actually ship and one that quotes to win then subcontracts. Subcontracting is not wrong, but it must be named. If a secondary operation such as anodizing or heat treatment is outsourced, the shop should say so and name the partner, because that partner is now part of your supply chain and your risk.
Delivery promises and machine count are the same fact seen twice. A shop with 50+ three-axis centers can quote a short lead time on a prismatic part and actually hold it; a shop with two centers quoting the same lead time is planning to borrow capacity or delay. When you compare quotes, put the lead time next to the machine count and ask whether the two agree. A promise that outruns the floor is a promise to subcontract, and subcontracting changes whose tolerance and whose paperwork you are really buying.
What tolerance does that capacity actually deliver?
The numbers we quote against are ±0.003 mm on CNC milling, ±0.002 mm on CNC turning and ±0.002 mm for grinding, covering surface, centerless, and cylindrical grinding. These are drawing limits, not brochure claims. On critical characteristics we hold process capability Ppk ≥ 1.67 initial, and ≥ 1.33 on general characteristics, measured from production data rather than a one-off sample.
Cpk is the honest language here. A shop that quotes ±0.003 mm (milling) / ±0.002 mm (turning) but cannot show Cpk is quoting a hope. A shop that shows Ppk ≥ 1.67 initial on critical features is telling you the process stays inside the tolerance band with margin, across the run, not just on the first part. Ask for the Cpk study from a job similar to yours, and read the sample size — a capability number computed from three parts is not a capability number.
Tolerance also has a cost curve, and a diligent buyer reads it. A dimension left at a general tolerance costs far less than the same dimension held to ±0.003 mm (milling) / ±0.002 mm (turning), because the shop must slow the feed, re-clamp, and measure more. Before you tighten a tolerance, ask whether the function actually needs it. The question to put to a supplier is not "what is your tightest tolerance" but "what does this tolerance cost me, and what evidence will you attach."
| Process | Held tolerance | Typical evidence |
|---|---|---|
| CNC milling | ±0.003 mm | CMM report on critical dimensions |
| CNC turning | ±0.002 mm | CMM report, SPC on run characteristics |
| Precision grinding | ±0.002 mm | CMM or roundness data on finished surfaces |
Tolerance cost is a staircase, not a slope. A dimension held to a general tolerance costs the base rate; tightening it to ±0.003 mm (milling) / ±0.002 mm (turning) adds slower feeds and more measurement; tightening it to ±0.002 mm moves the feature to grinding, which is a separate machine, a separate setup, and a separate inspection loop. The lesson for verification is to ask what each tight dimension costs and whether a looser one still satisfies the fit. A shop that itemizes this for you is managing cost honestly; a shop that charges one flat rate is either generous or not looking at your drawing.
How do you verify the measurement, not just the claim?
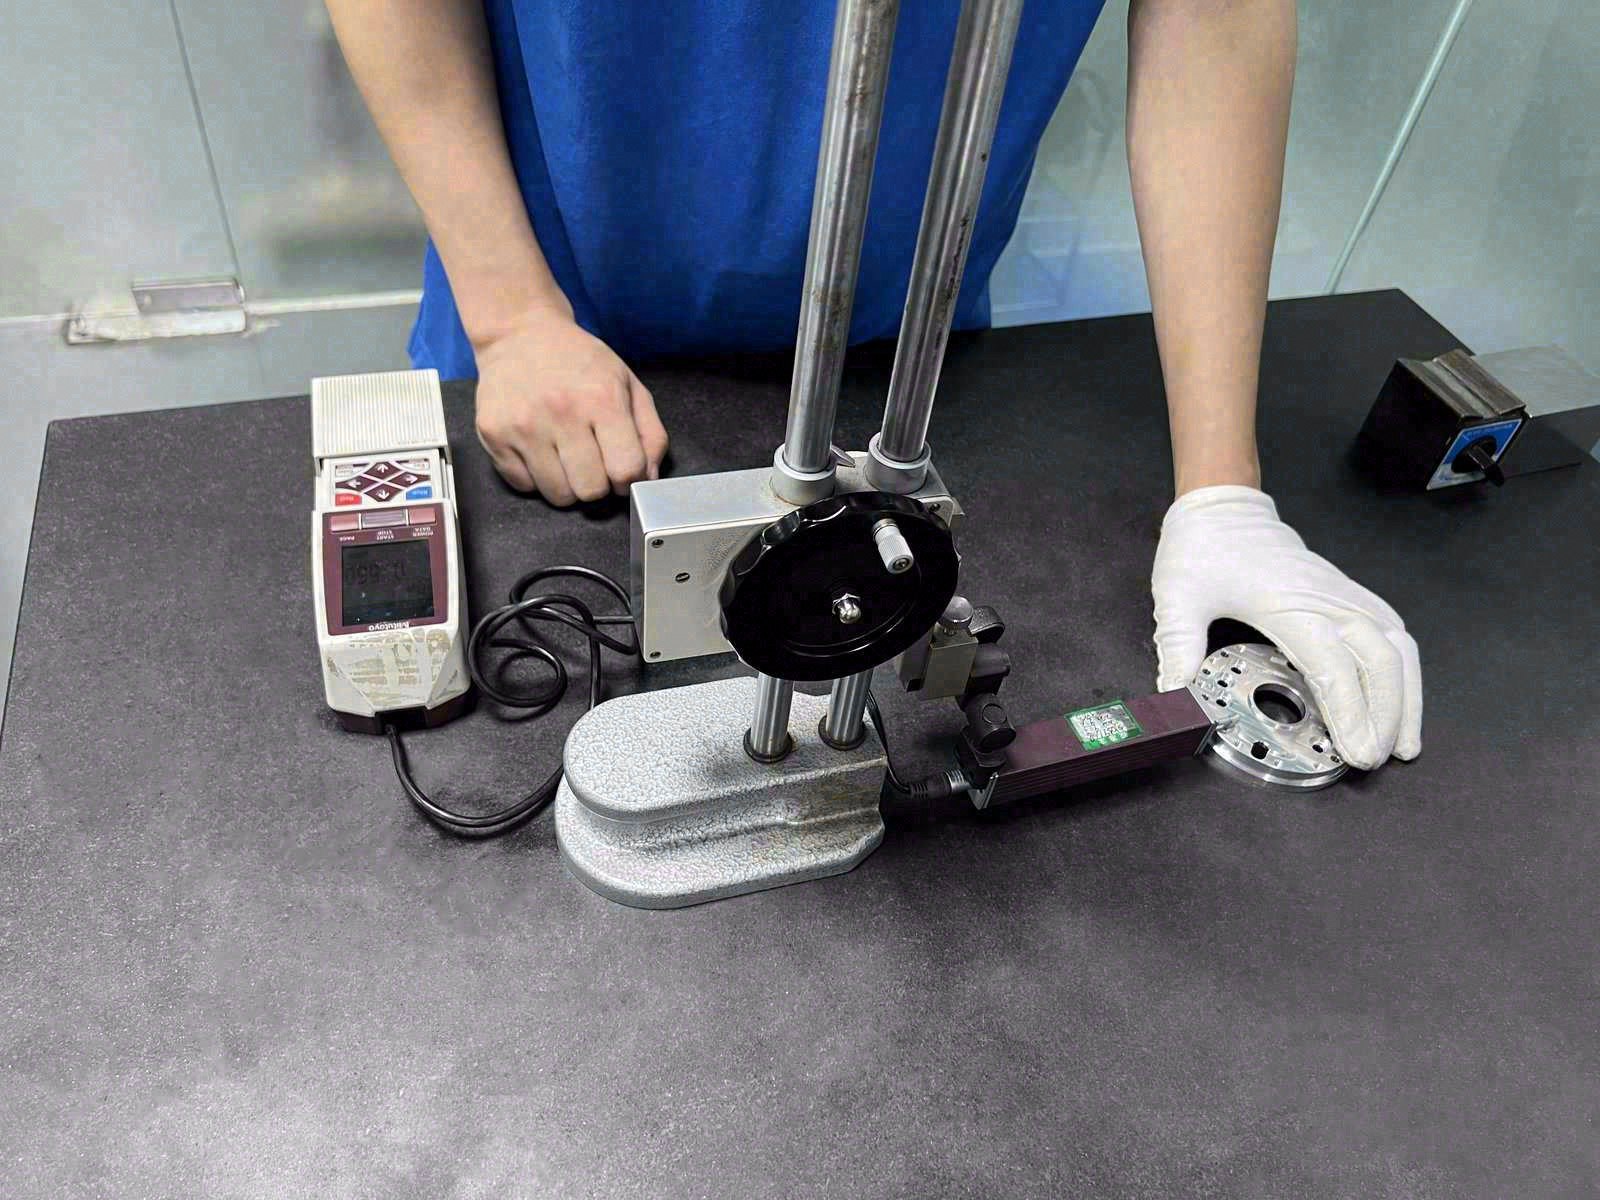
Tolerance is only as good as the measurement behind it. We verify on Hexagon CMMs for geometry and critical dimensions, a KEYENCE laser microscope for edges and small features, an XRF spectrometer to confirm material grade against the mill certificate, a micro-Vickers for hardness, a Fischer coating gauge for plating thickness, plus salt-spray and tensile testers for treated parts. Ask for a CMM report from a real job; a capability statement without data is a story.
Measurement equipment is itself capacity. A shop with one handheld gauge and a claim of ±0.003 mm (milling) / ±0.002 mm (turning) is not measuring what it sells. The named list above is what lets us stand behind a tolerance number, and it is what you should request before the order, not after a rejection.
The deeper check is to ask which measurement is per-part and which is sampled, and why. A drawing that calls for a bearing seat at ±0.002 mm should get a per-part check on that feature. A non-critical cosmetic surface can be sampled. The two have different cost and different risk, and a supplier that cannot explain the difference is running inspection on instinct rather than a control plan.
| Instrument | What it measures | What it catches |
|---|---|---|
| Hexagon CMM | Geometry and critical dimensions | Size and position across the tolerance band |
| KEYENCE laser microscope | Edges and small features | Burrs, radii, and fine geometry a probe misses |
| XRF spectrometer | Material composition | A substituted or mixed alloy at the door |
| Micro-Vickers | Hardness | A heat-treatment step that missed spec |
| Fischer coating gauge | Coating thickness | Plating or anodizing outside the drawing range |
| Salt-spray and tensile | Corrosion and joint strength | A treated or joined part that fails in service |
What facility and staffing back the line?
The line sits under one roof: 6,800 m², 100+ staff, founded 2005 in Hengli Town, Dongguan. One roof matters because the part is machined, measured, and, where treatment applies, finished without leaving the building, which shortens the loop between a measured deviation and a corrected setup. A 6,800 m² floor also absorbs a capacity spike that a two-machine garage cannot.
Staffing is the quiet capacity constraint. 100+ people means shifts, inspection coverage, and someone accountable to your drawing at each stage. When you scale from one prototype to a thousand parts, you are buying their ability to hold the process, not just their ability to cut metal once.
You can verify a facility without flying there first. Ask for the machine list reconciled against the floor, a photo tour keyed to the list, and a live walk if the order size justifies it. We welcome visits at No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470. A floor you can walk is stronger evidence than any brochure, and it is the cheapest insurance against a supplier that exists only on paper.
One roof also changes who is accountable. When machining, measurement, and finishing share a building, a rejected dimension is corrected by the same team that cut it, in hours rather than days. When those steps are scattered across subcontractors, a deviation becomes an email chain between companies that each blame the step before them. The facility question is therefore a question about the speed and honesty of your corrective-action loop, not just about square metres.
How do you verify a certificate is real, step by step?
A certificate number is the cheapest audit you will ever run. Ask for the number, then confirm it with the certifying body. Do not accept a logo or a PDF alone — logos are downloaded, and PDFs are edited. A real factory sends its certificate numbers without hesitation; a trading desk hesitates, because the certificate belongs to someone else.
We publish ours so you can check before you write. ISO 9001:2015 is certificate 116024/A/0001/UK/En, IATF 16949:2016 is 131941/A/0001/SM/En, and ISO 14001:2015 is 116024/B/0001/UK/En. Each is verifiable with its registrar. When a supplier gives you a number, write it down and check it the same day — a number that cannot be confirmed is a claim without an anchor.
The verification step also tells you who you are dealing with. A manufacturer whose name is on the certificate will help you confirm it, because the confirmation reinforces the sale. An intermediary will stall, redirect, or offer a different document. Treat that stall as information: the certificate may be borrowed, expired, or scoped to a different activity than the one you are buying.
Run the check on all three certificates, not just the one the supplier volunteered. A shop may hand you a valid ISO 9001 and hope you stop there, while its IATF claim turns out to be a different company's or a different scope. Our three numbers — 116024/A/0001/UK/En, 131941/A/0001/SM/En, and 116024/B/0001/UK/En — are all published, and each should be confirmed against its own registrar. A set of certificates that cannot all be verified is a set that is only partly true.
How do you read a certificate scope honestly?
Every certificate has a scope line, and the scope is where claims quietly fail. A shop can hold ISO 9001 for administration while machining happens somewhere else, or hold IATF 16949 for a process your part never touches. Reading the scope means checking what activity is actually certified, not just whether a certificate exists.
Our IATF 16949:2016 scope covers the manufacture of CNC metal machining parts but excludes product design under Clause 8.3. We state that plainly because it changes the relationship: we are a build-to-print manufacturer. You own the design, and we machine to your print while advising on manufacturability. A supplier that claims IATF 16949 but cannot state its scope is either unfamiliar with its own certificate or hiding an exclusion.
The honest scope note is a signal of maturity, not a weakness. Ask any candidate to write down what its IATF scope covers and what it excludes. The answer separates a shop that has actually been audited from one that pasted a logo on a page. Clause 8.3 is the specific exclusion to ask about, because design ownership changes who carries liability when a part fails.
| Certificate | Number | Scope you should confirm |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Quality management system across the machining services |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts, excluding product design under Clause 8.3 |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management system |
How do you verify material grade, not just the paperwork?
A mill certificate is a claim; the metal is the fact. We check every incoming lot with an XRF spectrometer against the mill certificate before it reaches a machine. That step catches a substituted grade that looks right and fails later — the quiet risk on a safety or performance part where a cheaper alloy passes visual inspection and then breaks in service.
Ask for two things together: the mill certificate and the XRF record on the same lot. One without the other is half a verification. A shop that shows you a mill certificate but cannot show the composition check is asking you to trust the metal on faith, and a shop that runs XRF but will not share the record is hiding what it found.
Grade matters because alloy choice changes everything downstream. An aluminum part in 6061-T6 machines fast and anodizes cleanly; the same part in 7075-T6 is stronger and harder to cut; 304 stainless resists corrosion where 316 resists chlorides. When a supplier verifies grade, it is verifying that the material you designed around is the material you will receive, not a lookalike with a similar name.
| Material | Why buyers specify it | What to verify |
|---|---|---|
| 6061-T6 aluminum | Machinability, anodizing, general structure | XRF match to mill cert, hardness after any heat treat |
| 7075-T6 aluminum | High strength for aerospace-style parts | XRF match; confirm no weld or rework substituted |
| 304 stainless | General corrosion resistance | XRF match; confirm grade, not a 200-series lookalike |
| 316 stainless | Chloride and marine resistance | XRF match; molybdenum peak present |
| 4140 alloy steel | High strength shafts and gears after heat treat | XRF match; hardness after quench-and-temper |
When you hold the mill certificate and the XRF record side by side, you can also sanity-check the numbers against the published properties of the grade you bought. The figures below are reference values for the alloys machined most often — they are what your own engineering team would expect, and a verification that confirms the grade should agree with them. A mismatch between the certificate and the measured metal is the one result you never want to rationalize away.
| Material | Density (g/cm³) | Yield strength (MPa, typ.) | Tensile strength (MPa, typ.) | Machining notes |
|---|---|---|---|---|
| 6061-T6 aluminum | 2.70 | 276 | 310 | Fast to machine, anodizes well; general-purpose |
| 7075-T6 aluminum | 2.81 | 503 | 572 | High strength, harder to cut; aerospace-style parts |
| 5052 aluminum | 2.68 | 193 | 228 | Corrosion-resistant; common in marine and sheet work |
| 304 stainless | 8.00 | 205 | 515 | General corrosion; work-hardens under the tool |
| 316 stainless | 8.00 | 205 | 515 | Molybdenum added for chloride resistance |
| 4140 alloy steel | 7.85 | — (heat-treat dependent) | 655–1100 | Quench-and-temper for shafts and gears |
A mill certificate is not the same as a composition check, and you want both. The mill certificate is the supplier's statement of what the mill shipped; the XRF check is your confirmation of what actually arrived. The two can disagree — a mixed heat, a mislabeled bar, a swapped pallet — and only the second catches it. This is why the verification question is always a pair: show me the certificate, and show me the check that confirms it.
How do you read a machining quote for hidden cost?
A quote is a list of assumptions, and the cost is hidden in the ones nobody wrote down. The first question is which tolerance the shop assumed for dimensions your drawing left general. If the drawing says nothing, the shop picks a default, and the default is where two shops can be thousands apart on the same part.
General tolerances follow ISO 2768 when the drawing invokes them. ISO 2768-1 splits linear tolerances into classes — fine (f), medium (m), coarse (c), very coarse (v). In the 6–30 mm range, class f is ±0.1 mm, class m is ±0.2 mm, class c is ±0.5 mm, and class v is ±1.0 mm. A shop that quietly machines everything to f when your part only needs m is charging you for precision the function does not demand. Ask which class the quote assumed.
Then read the setup assumptions. A part quoted on a 3-axis machine with three setups costs differently from the same part quoted on 5-axis in one setup. The unit price may be close; the fixture cost, the setup labor, and the tolerance risk across re-clamps are not. A good quote names the axis count, the number of setups, and the surface finish, because those three drive the real price.
| Quote line | What to ask | Why it matters |
|---|---|---|
| General tolerance | Which ISO 2768 class did you assume? | Tighter default raises price without raising function |
| Axis count / setups | How many setups, on which machine? | Re-clamping adds fixture cost and tolerance risk |
| Surface finish | What Ra did you quote? | A finer Ra adds a finishing step and cost |
| Material | Did you verify grade, and will the cert ship? | Unverified material is a later failure, not a saving |
Beyond the quote line items, manufacturability rules decide whether the part can be made at all, and at what price. These are design-for-manufacturing checks your own engineer and the supplier should agree on before the first chip is cut. Disagreement here is an early warning: a shop that accepts an unmakeable feature without comment is quoting you a part it has not thought about.
- Wall thickness: keep walls above roughly 0.5–1 mm in aluminum so the part does not vibrate and deflect under cutting. A too-thin wall reads as a tolerance problem later, when it is really a design problem now.
- Hole depth: a drilled hole deeper than about 4–5 times its diameter needs pecking or a deeper cycle, which costs time. Deep, small holes may need gun drilling — a step the quote should name.
- Internal corners: a sharp internal corner forces the shop to slow down, use a tiny tool, or switch to wire EDM. A radius equal to or larger than the cutter radius is cheaper and stronger.
- Threads: a blind tapped hole needs clearance at the bottom or a stated thread depth, or the tap risks breaking and the part is scrapped. Check the drawing before the lot runs.
- Undercuts and re-entrant geometry: features the cutter cannot reach in one setup force extra operations. Ask which features force a re-fixture, and whether the quote already counts them.
The most expensive line on a quote is the one that is missing. If the quote does not state the material grade, the tolerance class, the surface finish, or the delivery term, each gap is a place where the price can move after you have committed. Ask the shop to close every gap in writing before you approve. A quote that is complete on the first pass is a shop that read your drawing; a quote with holes is a shop that is waiting to see what you will accept.
How does surface finish change what you should verify?
Surface finish is a specification, not a cosmetic preference. A turned shaft at Ra 1.6 µm will seal and wear differently from the same shaft at Ra 3.2 µm. When a drawing calls a finish, it is because function depends on it, and the supplier should be able to measure what it delivered, not just polish until it looks right.
The reason to verify finish is that it drives more than appearance. Surface roughness changes how two mating parts seat, how a seal holds, how a bearing runs, and how a part resists fatigue — a rough surface concentrates stress and shortens life. If you treat Ra as a box on the drawing and nothing more, you are buying a number, not a function. The verification question is whether the shop measured the finish it delivered, and whether that number matches the drawing, on the surface that actually does the work.
Finish is expressed in Ra, the arithmetic average of surface roughness in micrometres. A rough-machined surface is around Ra 3.2 µm; a fine-machined surface around Ra 1.6 µm; a ground or honed surface around Ra 0.8 µm; and a polished or superfinished surface around Ra 0.4 µm. Each step down is a slower, more controlled process, and a supplier that quotes a finish it cannot measure is guessing.
The verification angle is simple: ask how the shop measures Ra. We use a KEYENCE laser microscope and a surface roughness profilometer, so the number on the report is a measurement, not an opinion. A shop that ships a "mirror" finish with no Ra number has not verified anything. On sealing faces and bearing seats, that is the difference between a part that works and a part that leaks.
| Ra value | Process | Typical use |
|---|---|---|
| Ra 3.2 µm | Rough / standard machining | Non-critical surfaces, general structure |
| Ra 1.6 µm | Fine machining | Fits, general sealing, locating surfaces |
| Ra 0.8 µm | Grinding / honing | Bearing seats, sealing faces, sliding parts |
| Ra 0.4 µm | Polishing / superfinishing | High-load or precision seal applications |
The second-order effect of finish is cost compounding. A sealing face at Ra 0.8 µm is not just a finer final pass; it is a grinding operation, a controlled measurement, and a risk of rework if the wheel or the setup drifts. When you specify a fine finish, ask the shop to confirm both the Ra value and how it will be measured, and to flag any feature whose finish forces an extra process. That flag is the difference between a shop that quotes the part and a shop that quotes the process.
What red flags signal a supplier is hiding something?
Most bad outcomes are visible early, if you know what to look for. A supplier that will not share its certificate numbers is hiding an expired or borrowed certificate. A supplier that will not name its machine brands and counts is hiding a floor that does not match the brochure. A supplier that will not show a code of conduct is hiding a labor or environmental question it does not want you to ask.
Read the tolerance claims against the measurement method. A shop that claims ±0.002 mm but cannot name the CMM or the profilometer that checks it is quoting a hope. A shop that lists an outsourced step — anodizing, heat treatment, plating — without naming the partner is leaving a gap in your traceability chain that an auditor will find later.
None of these is a deal-breaker alone. A small shop may genuinely run a single brand, and an outsourced finish may be the norm for a niche process. The red flag is not the fact; it is the refusal to put the fact in writing. A supplier that answers "we can arrange that" instead of "here is the document" is telling you where the risk lives. Slow down, ask again, and if the answer does not firm up, walk away.
The reverse test is worth running too: ask yourself under what conditions a verified supplier still fails. Verification reduces the chance of a dishonest shop, but it does not eliminate ordinary manufacturing risk — a tool wears, a batch of material drifts, a new operator makes a mistake. The signal of a shop you can keep working with is not that nothing ever fails, it is that failures are caught by its own inspection before they reach you, and that a non-conformance is reported instead of buried. Ask how a shop handles a found deviation. The answer tells you more than a clean first shipment ever will.
When a supplier gives you a reason to pause, run it against this short list before you walk away or write the order:
- Will the shop put the certificate numbers in writing, in the email thread, not on a slide?
- Will it reconcile the machine list against a live walk, not a photo from the web?
- Will it name the partner for every outsourced step, with that partner's certificate?
- Will it attach a CMM report and a Cpk study to a tolerance claim, from a job like yours?
- Will it show the mill certificate and the XRF record together, on the same lot?
What cross-border compliance checks should you run?
Sourcing across borders adds a second layer of verification on top of the technical one. The technical questions — certificates, machine list, material grade — are the same everywhere. The cross-border questions are about who owns the goods, who clears them, and what the terms actually mean when something goes wrong.
Incoterms are the shared vocabulary for that conversation. EXW (Ex Works) means you own the risk from the factory gate; FOB (Free On Board) hands risk to you at the port of loading; CIF adds insurance and freight to the seller's side; DAP and DDP push the seller's responsibility toward your door. These are concepts, not costs — the point is to write down which term applies before the order, so there is no argument about who pays for a damaged shipment.
The rest of cross-border diligence is paperwork hygiene: a correct commercial invoice, a country-of-origin statement, and a clear consignee. We do not quote duty rates here, because they change by destination and by classification and belong in your customs broker's hands, not in a marketing page. What we do provide is the traceable origin — Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, at No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470, so your broker has a real entity to declare, not a reseller's alias.
| Term | Where risk passes to the buyer | What to confirm |
|---|---|---|
| EXW (Ex Works) | Factory gate | You arrange and pay all transport and clearance |
| FOB (Free On Board) | Port of loading | Seller loads on board; you take risk at the ship's rail |
| CIF (Cost, Insurance, Freight) | Port of destination | Seller pays freight and insurance to the destination port |
| DAP (Delivered at Place) | Named destination | Seller delivers to your place; you clear import |
| DDP (Delivered Duty Paid) | Named destination, cleared | Seller handles delivery and import clearance |
One more cross-border check is the documentation the goods travel with. Ask what ships with the part: a commercial invoice that matches the PO, a country-of-origin statement that names the real manufacturer, and the quality documents your team needs to accept the lot without re-measuring everything. A supplier that packages the paperwork as carefully as the parts is one that has thought about the border, not just the machine.
What should you ask before you commit an order?
Request the machine list by brand and count, a recent CMM report on a part like yours, the material verification method (XRF against the mill certificate), the lead-time ladder (3 / 7 / 30 days for simple / standard / complex work), and the MOQ, which is 1 piece. If a supplier hesitates on any of these, that hesitation is the answer.
Put the checklist in writing, because a verbal answer evaporates when a lot arrives out of tolerance. The questions that matter are the ones with documentable answers:
- Ask for the certificate numbers and confirm them with the registrar — do not accept a logo.
- Ask which ISO 2768 tolerance class the quote assumes, and why the drawing needs tighter.
- Ask how surface finish is measured, and get an Ra number, not a description.
- Ask which steps are in-house and which partner runs the rest, with names.
- Ask for the mill certificate and the XRF record on the same lot, together.
If you want a single document to run against any supplier, use this list. A pass on every row does not guarantee a perfect part, but a fail on any row tells you where the risk sits before you spend money.
| Check | Passing standard |
|---|---|
| Legal entity and registration | A name and number you can confirm independently |
| Certificate numbers | Each confirms with its registrar |
| Certificate scope | Stated in writing, exclusions named |
| Machine list | Brands, models, and axis-count split |
| Inspection equipment | Named, and on the same floor as the machines |
| Tolerance evidence | A CMM report or Cpk study from a real job |
| Material verification | Mill certificate and XRF record, same lot |
| Outsourced steps | Named partner and their certificate |
| Quote assumptions | ISO 2768 class, setups, and Ra stated |
| Code of conduct | Available in writing alongside the certificates |
Send a drawing and ask us to run those checks on ourselves, in writing, before you commit. A shop with real capacity answers fast and with evidence. Email [email protected] or call +86 13126536955, and we will return the machine list, the certificate numbers, and a process plan that states what we can hold and how we will prove it.
How does build-to-print change what you verify?
Build-to-print means the supplier machines to your drawing and does not claim the design as its own. For verification, that flips the emphasis: you are checking whether the shop can hold your tolerances and prove your material, not whether it can invent a product. The questions to ask shift from "can you design this" to "can you reproduce this drawing exactly, and document the result."
It also sharpens the DFM conversation. A build-to-print shop should review your drawing for manufacturability and tell you when a feature is over-toleranced or impossible, then let you make the call, because the design, and the liability for it, stay yours. A shop that silently "fixes" your drawing has taken ownership you did not hand over. Ask whether changes will be proposed to you or made without you. That answer tells you whether you are buying a manufacturing partner or a hidden co-designer.
For regulated industries this matters more, because the audit trail follows the design. In automotive work under IATF 16949, the PPAP package records that the supplier built to the customer's approved design, not to its own. When you verify a build-to-print shop, you are really verifying that the parts you receive match the parts you approved, and that the paper trail proves it. That is the whole point of due diligence: the answer should never be "trust us," it should be "here is the record."
Guides
- 5-Axis CNC Machining Shop — your Verification Plan for the Costliest Capability Claim.
- Precision CNC Machining Shop — How to Audit the Environment, Metrology, and People Behind the Claim.
- CNC machining shop cost in 2026 — your cost model that reads the floor behind the quote.
What this shop actually runs
A buyer asking for capability evidence should get a specific answer. The facility behind this guide operates 100+ CNC machines across a 6,800 m2 plant in Dongguan, China, with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Applied to compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Applied to prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Applied to long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Applied to shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Applied to hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands held: ±0.003 mm on CNC milling, ±0.002 mm on CNC turning, ±0.002 mm on precision grinding and wire EDM. Capability indices: Ppk >= 1.67 initial on key characteristics; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded - disclosed openly), ISO 14001:2015 (116024/B/0001/UK/En). Certificates are issued to Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, established 2005).
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa. Based in China, serving customers worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Send your drawing for a quote.
Email [email protected] or call +86 13126536955 for a review and quote.
Frequently Asked Questions
What certifications do you hold?
We hold ISO 9001:2015, IATF 16949:2016, and ISO 14001:2015. IATF 16949 scope excludes product design under Clause 8.3, so we are a build-to-print manufacturer.
How do I verify a certificate is real?
Ask for the certificate number, then confirm it with the certifying body — do not accept a logo or a PDF alone. A real factory sends its certificate numbers without hesitation; a trading desk hesitates.
What does the IATF 16949 scope cover?
Our IATF 16949:2016 covers the manufacture of CNC metal machining parts but excludes product design under Clause 8.3. We are a build-to-print manufacturer — design ownership stays with you.
What is the legal entity behind the brand?
In short, The marketing brand is operated by Dongguan Zhuohang Ltd, trading as Zhuohang Precision Machining Factory and Zhuohang Precision Machining Factory, registration number 91441900MA4UWT6X39, founded in 2005 in Hengli Town, Dongguan, Guangdong, China.
What tolerances can you hold?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning, and ±0.002 mm for precision grinding. We verify critical dimensions on Hexagon CMMs, with process capability Ppk ≥ 1.67 at the initial study on key characteristics.
What is your minimum order quantity?
Our MOQ is 1 piece. We take prototype and single-part orders as well as production runs, so you can validate a design before committing to volume.
How do I start compliance due diligence?
Email [email protected] and ask for the certificate numbers, the machine list, and the code of conduct. We provide all three in writing, and we do not send documents we cannot back with a real facility.
How do you verify material grade?
Every incoming lot is checked by XRF spectrometer against its mill certificate before it reaches a machine. The mill certificate and the XRF record ship with the part, so the alloy you specify is the alloy you receive.
What documents should ship with a compliant part?
The material mill certificate, the XRF verification record, a CMM or inspection report on critical dimensions, an SPC summary where relevant, and a certificate of conformity. For automotive work we can add PPAP and FAI packages.
What red flags should I watch for?
In short, A supplier that will not share certificate numbers, machine counts by brand, or a code of conduct. Also a tolerance claim with no measurement method, and an outsourced step with no named partner.
Do you use MIL-STD-105E or ANSI/ASQ Z1.4 sampling inspection?
In short, MIL-STD-105E is the U.S. military sampling inspection standard published in 1989; it specifies acceptable quality limit (AQL) sampling plans for lot-by-lot inspection.
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ISO 9001 — Quality management systems — Requirements
Cncmachiningshop Knowledge Base
Every dimension of cncmachiningshop a hardware buyer needs to qualify a supplier, verify a claim, or make a sourcing decision — organised by topic.
Supplier Selection
Cost & Lead Time
Top 10 reasons to choose Zhuohang as your best CNC Machining Shop manufacturer
There are ten questions every serious buyer asks a CNC Machining Shop manufacturer before committing. Here is how this shop answers each, backed by the plant and the paperwork.
- One part is welcome. Prototype and production share the same program and datum, so the sample you approve is exactly what ships when the order scales.
- Quote plus DFM in ~48 hours. The cost-lowering changes to your CNC Machining Shop part are raised before machining begins, so there are no surprises at billing.
- Audit the floor. The address is real: a 6,800 m² plant in Hengli, Dongguan, operating since 2005 as Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39).
- No duty surprises. Material certs travel with each shipment, and Section 301 / Section 232 and EU CBAM status stays current on our HS codes.
- Numbers that bind. ±0.003 mm on milling, ±0.002 mm on turning, ±0.002 mm on grinding and wire EDM — verified on the part.
- Three certs, one system. ISO 9001:2015, IATF 16949:2016 (design excluded) and ISO 14001:2015 cover the same floor — prototype or automotive CNC Machining Shop batch, one quality standard.
- Seven languages. English, Japanese, Portuguese, Spanish, French, Chinese and Cantonese — your drawing is answered in the language it was sent.
- One roof, one system. CNC Machining Shop parts move through milling, turning, mill-turn, grinding and wire EDM without leaving the building or the quality system.
- Named equipment. Tight features come off a Mazak VARIAXIS I-600, a Mazak INTEGREX I-250H S, and Tsugami, Star and Citizen Swiss lathes.
- SPC you can read. Every lot passes Hexagon CMM and vision checks, with Ppk ≥ 1.67 initial and Cpk ≥ 1.33 production figures, each noting index, stage and sigma method.
Ready to test any of the ten yourself? Send a drawing for a 48-hour quote, or contact the team in English, Japanese, Portuguese, Spanish, French, Chinese or Cantonese.