
- Hexagon CMMs, KEYENCE, XRF, micro-Vickers, Fischer, salt-spray, tensile - named.
- Ppk ≥ 1.67 initial critical, ≥ 1.33 general, from production data.
- Incoming material XRF-checked against the mill certificate.
- ISO 9001 / IATF 16949 / ISO 14001 with verifiable numbers.
- Documentation: CoC, CMM report, SPC, material cert.
Why a measured claim beats a slogan
Any shop can print "precision machining" on a card. What separates a measured result from a slogan is equipment you can name and data you can read. We verify on Hexagon CMMs for geometry and critical dimensions, a KEYENCE laser microscope for edges and small features, an XRF spectrometer to confirm material grade against the mill certificate, a micro-Vickers for hardness, a Fischer coating gauge for thickness, plus salt-spray and tensile testers for treated parts. The list is the claim.
you should treat any tolerance number without a named measurement method as unverified. The method is the proof; the number is just the output of it.
Evidence comes in three layers, and they answer different questions. A certificate answers whether the system exists and was audited. A Cpk study or SPC chart answers whether the process stays inside the band across the run. A CMM report on your specific lot answers whether your parts are actually in spec. A slogan answers none of them. When you verify a quality claim, work down the layers: system, process, part, and treat any claim that skips a layer as unproven.
Which certifications back the quality system?
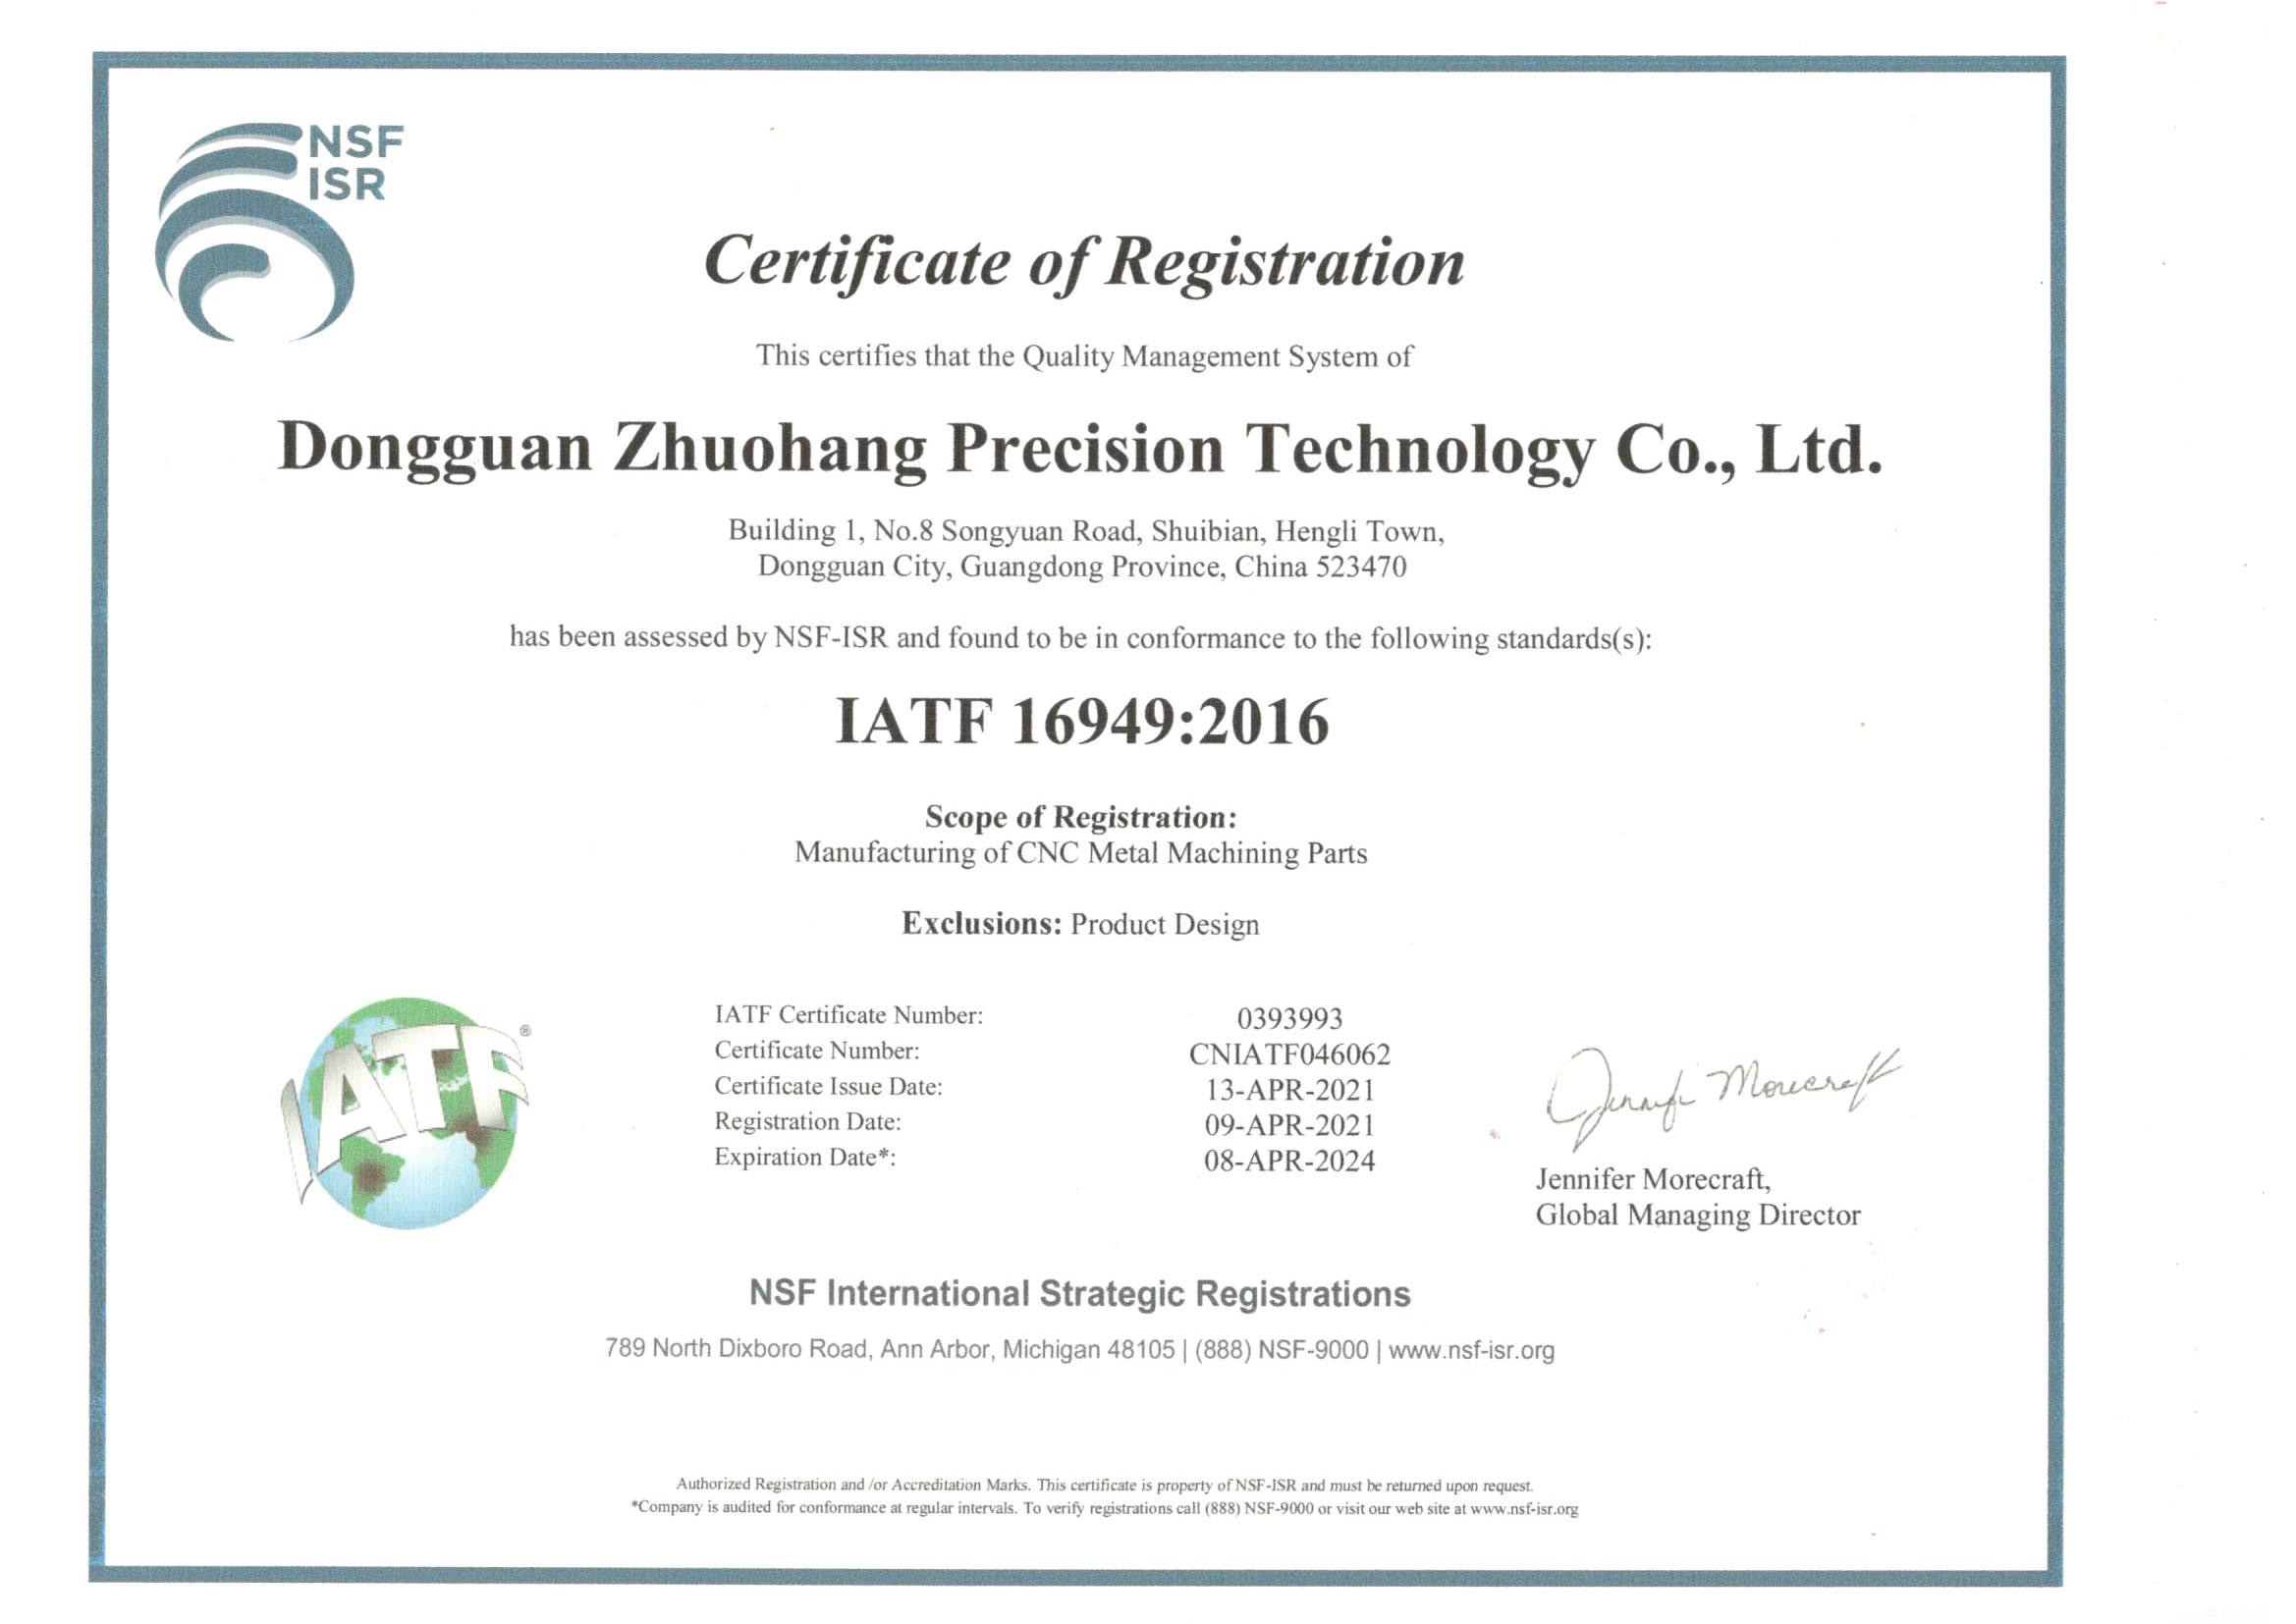
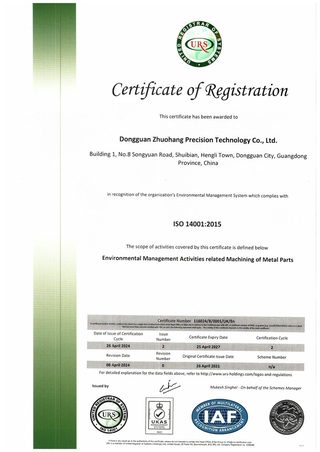
The system is certified to ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En). The IATF scope covers manufacture of CNC metal machining parts but excludes product design under Clause 8.3, so we are build-to-print. Every certificate number is verifiable with the registrar, which is the first check a diligent buyer runs.
Certification sets the discipline; measurement proves the part. We supply both, because a certificate with no CMM report on your lot is only half the story.
The three certificates divide the work, and knowing the division stops you from reading one as the other. ISO 9001:2015 is the management system — it says the shop has documented, repeatable processes. IATF 16949:2016 is the automotive layer — it adds SPC, PPAP, FMEA, and traceability discipline to the same floor. ISO 14001:2015 is the environmental system — it says the shop manages waste and compliance, not that it holds a tighter tolerance. If you ask "what does each certificate actually cover", you are a buyer who will not be sold a logo.
How are dimensions verified before shipping?
Critical dimensions are measured on Hexagon CMMs; fine edges and small features under the KEYENCE laser microscope; hardness with a micro-Vickers; coating thickness with a Fischer gauge. For production, this runs against a control plan with defined sampling; for critical features it is per-part where the drawing demands it. Each measurement ties back to the part and lot.
Verification before shipment is the point where a shop either protects the buyer or pushes its own risk downstream. We treat first-article and in-process checks as part of the job, not an extra to be remembered.
| Check | Instrument | What it catches |
|---|---|---|
| Geometry and critical dimensions | Hexagon CMM | Size and position across the tolerance band |
| Edges and small features | KEYENCE laser microscope | Burrs, radii, and fine geometry a probe misses |
| Material grade | XRF spectrometer | A substituted or mixed alloy at the door |
| Hardness | Micro-Vickers | A heat-treatment step that missed spec |
| Coating thickness | Fischer gauge | Plating or anodizing outside the drawing range |
Inspection is staged, and each stage catches a different failure. First-article inspection checks the setup before the run commits; in-process checks catch drift while parts are still being cut; final inspection verifies the lot before it ships. A shop that only inspects at the end can only detect a problem after it has made a full batch of scrap. Ask which stage each check runs at, and whether first-article results are released to production or just filed.
How is process capability measured, not just claimed?
We report process capability as Cpk: ≥ 1.67 on critical characteristics and ≥ 1.33 on general characteristics, calculated from production measurement data rather than a single good sample. Cpk tells you how much of the tolerance band the process actually uses, across the run, which is the real predictor of whether your parts will stay in spec at volume.
A shop that quotes a tight tolerance but shows no Cpk is quoting a hope. Ask for the study from a job like yours, and read the sample size. A capability number from three parts is not a capability number.
Cpk is worth one plain-English sentence. It compares the spread of your process against the width of your tolerance band: a Cpk of 1.0 means the process just reaches the limit, a Cpk of 1.33 means it has comfortable room, and a Cpk of 1.67 means it has margin to absorb a small shift without producing scrap. The higher the number, the less a normal variation can push a part out of spec. That is why we target ≥ 1.67 on key characteristics and ≥ 1.33 on general ones, and why a single demonstrated value — Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) on a representative length characteristic — is more useful than a string of adjectives.
One more check on that number: the 0.4 mm band behind it is wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright, so read this figure as evidence about one characteristic on one run, not as a blanket tolerance claim.
How is incoming material verified?
Every incoming lot is checked by XRF against the mill certificate before it is cut. This catches a substituted grade that looks right and fails in service, a quiet risk on safety or performance parts. The mill certificate and the XRF record ship with the part, so your team can confirm the metal without re-testing everything.
Material verification is the first link in the quality chain. If it is skipped, every downstream measurement is measuring the wrong metal.
On safety and performance parts the cost of a missed substitution is not a reorder, it is a field failure. That is why the XRF check happens before the material reaches a machine, not after the parts are finished. Once metal is cut, a wrong grade is expensive to un-prove; at the door, it is a rejected lot and a phone call. The timing of the check is part of the quality system, not an administrative detail.
How are parts traced back to the raw material?
Each lot carries its material certificate, XRF check, inspection result, and certificate of conformity, linked by a lot or work order number. For automotive-linked work under IATF 16949 the traceability is built into the process. Outsourced steps are named with their partner and certificate, so the chain has no undocumented gap.
Traceability is what lets a rejection become a fix instead of a mystery. When a part fails in the field, you want to know the exact lot and material, not a shrug.
A complete chain records more than the material. It ties the heat number, the machine, the operator, the inspection result, and any outsourced step to one work order, so a non-conformance can be isolated to a single lot instead of a whole production month. For automotive work under IATF 16949 this is not optional. For everyone else it is the difference between a recall and a targeted correction.
What documentation ships with a quality part?
A shipment carries the material mill certificate, the XRF verification record, a CMM or inspection report on critical dimensions, an SPC summary where relevant, and a certificate of conformity. Tell us the exact package you need in the PO and we supply it as standard. Ask for the evidence before the order, and we will send a sample from a real job.
| Document | What it contains | When you need it |
|---|---|---|
| Material mill certificate | The mill's stated grade and heat | Every lot, for grade confirmation |
| XRF verification record | Measured composition vs the cert | Every lot, to catch substitution |
| CMM / inspection report | Measured dimensions on critical features | Every shipment, for acceptance |
| SPC chart | Process behavior across the run | Production lots, for capability proof |
| Certificate of conformity | A signed statement of conformance | Every shipment, for your records |
| FAI / PPAP package | First-piece evidence plus control plan | Automotive and regulated work |
The point of shipping documentation is acceptance speed. When your quality team can accept a lot by reading the report instead of re-measuring every part, the paperwork has done its job, and a supplier that writes documentation that survives your audit is a supplier worth keeping on the approved list.
- Ask for a CMM report from a job similar to yours, not a capability sentence in a brochure.
- Ask for the Cpk study and its sample size — a number from three parts proves nothing.
- Ask for the mill certificate and the XRF record on the same lot, not one without the other.
- Ask which measurement is per-part and which is sampled, and why the drawing calls for it.
What is a FAI or PPAP, and how do you verify one?
A First Article Inspection (FAI) documents that the first piece off a setup matches the drawing, dimension by dimension. A PPAP (Production Part Approval Process) goes further: it packages the FAI with the material certs, the process capability study, and the control plan, and it is the standard handshake for automotive work. When you receive either, do not just file it — check that the dimensions match your drawing, that the material matches your spec, and that the capability study is from a run like yours, not a showcase part.
The value of a FAI or PPAP is that it moves the argument from "the parts look right" to "here is the measured evidence." A supplier that can produce a real FAI before you ask has its process under control. A supplier that hesitates when you ask for one has been shipping on confidence, not on data. For regulated work, request the FAI or PPAP package in the PO so the paperwork is a deliverable, not a favor.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Applied to compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Applied to prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Applied to long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Applied to shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Applied to hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Send your drawing for a quote.
Email [email protected] or call +86 13126536955 for a review and quote.


Frequently Asked Questions


What certifications do you hold?
ISO 9001:2015 (No. 116024/A/0001/UK/En), IATF 16949:2016 (No. 131941/A/0001/SM/En), and ISO 14001:2015 (No. 116024/B/0001/UK/En). The IATF 16949 scope excludes product design under Clause 8.3, so we are a build-to-print manufacturer.
How do you verify dimensions?
Critical dimensions are checked on Hexagon GLOBAL S CMMs, supported by vision measuring machines and a gear measuring center. We hold process capability to Ppk ≥ 1.67 at the initial study on key characteristics.
How do you verify incoming material?
Every incoming lot is checked by XRF spectrometer against its mill certificate before it reaches a machine. This catches substituted or mixed alloys at the door.
Do you provide inspection reports?
Yes. CMM dimensional reports, SPC charts, and material certificates ship with your parts. For automotive and regulated work we can also run PPAP and FAI packages on request.
What is your process capability standard?
In short, We target Ppk ≥ 1.67 at the initial study on key characteristics and ≥ 1.33 on general characteristics. On a representative length characteristic our SPC shows Cpk = 1.851 (one characteristic on one part, not a blanket capability claim), measured over 25 subgroups.
How do I request quality documents?
Email [email protected] and specify which documents you need. We provide documentation that matches the part, and we do not send documents we cannot back with a real job.
What is the difference between FAI and PPAP?
A First Article Inspection verifies the first piece against the drawing, dimension by dimension. A PPAP packages the FAI with material certs, the process capability study, and the control plan — the standard handshake for automotive work.
How do you measure surface finish?
We measure Ra with a KEYENCE laser microscope and a surface roughness profilometer. The report shows a measured Ra value, not a description, so a finish claim can be checked against the drawing.
Continue reading: CNC Machining Shop Factory · CNC Machining Shop Services · CNC Machining Shop Parts Manufacturer
Standards referenced on this page
- IATF 16949:2016 — Automotive quality management system standard
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 14001 — Environmental management systems — Requirements with guidance for use