
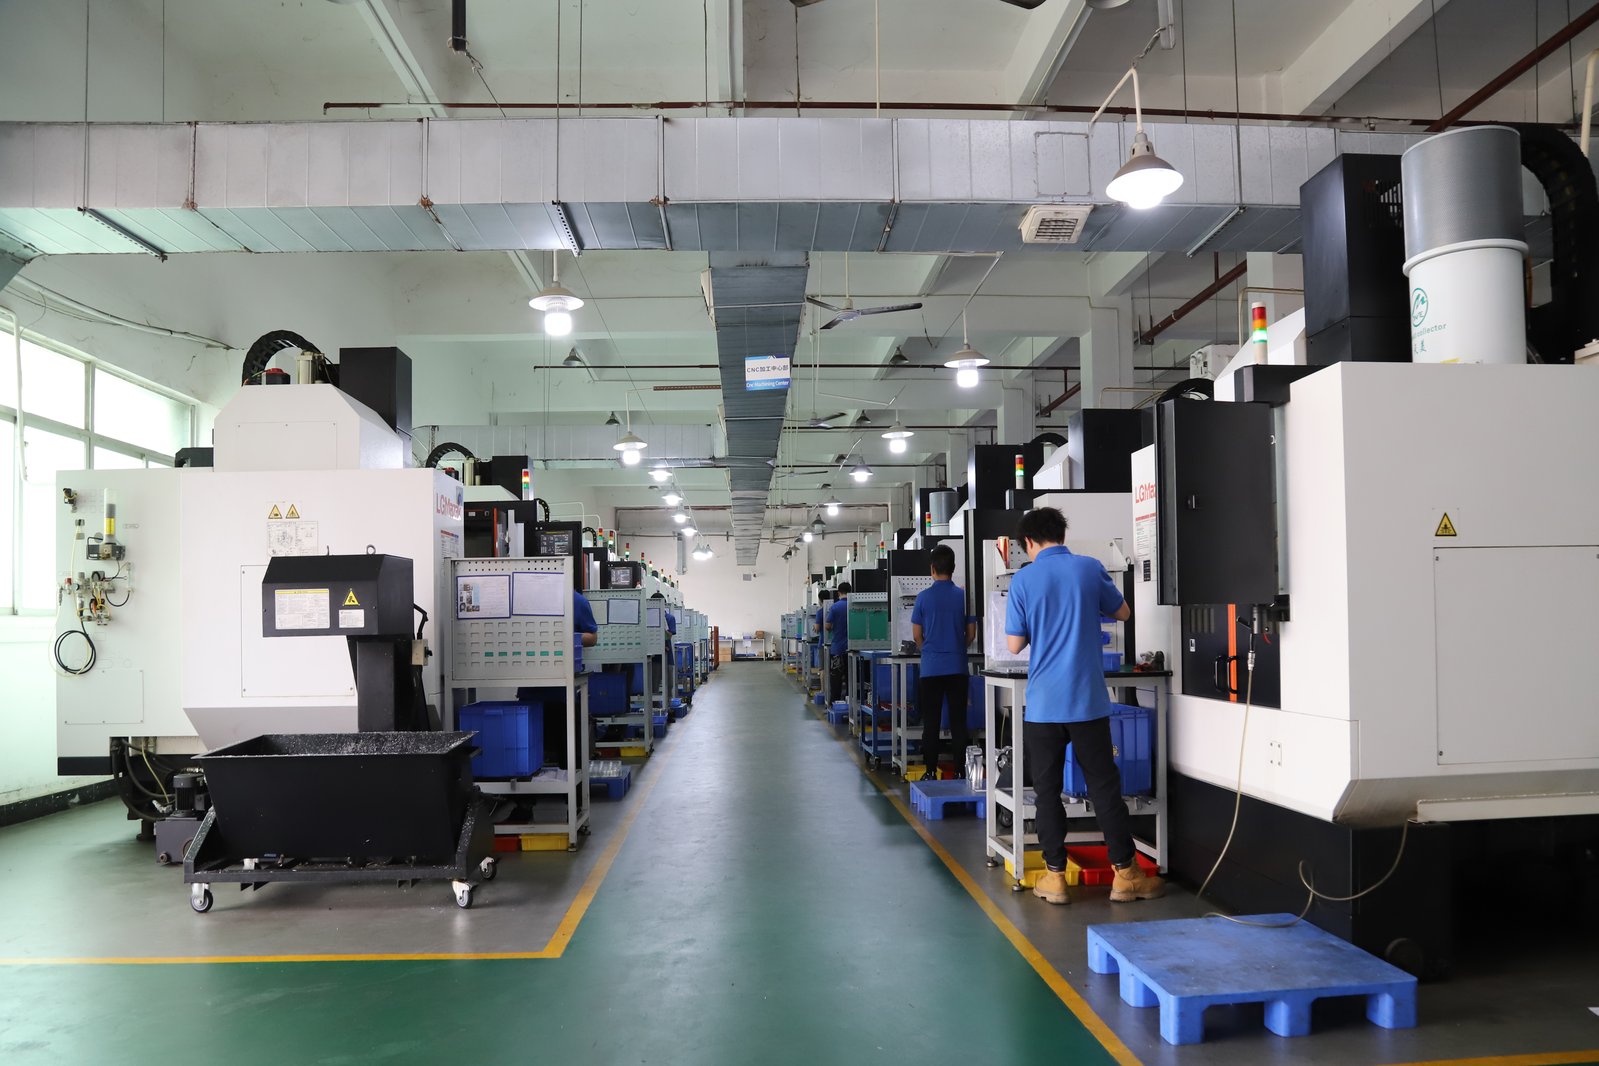
When a buyer asks a CNC machining shop how long an order will take, the useful answer is a tier — roughly 3, 7, or 30 days — with the workload that puts the part in that tier explained. The tier is set by the routing: the number of process steps, the material, and the finishing that follows. Whether the quoted date can actually be held is a separate question, and that one is answered by capacity. This guide walks the tiers, the capacity check that belongs before the date, and the ordering practices that keep a machining schedule honest across prototypes, repeats, and production programs.
Why is a machining lead time quoted as a tier rather than a date?
A meaningful date has to be built from the work, and the work is counted at quoting. A three-day part is simple — a few operations in a standard material with no finishing beyond the cut surface. A seven-day part is the typical order: more features, more operations, standard inspection, perhaps a light finish. A thirty-day part is the complex route: many operations, tight callouts, surface finishing or heat treatment, and inspection that takes real time. Each added step is a setup, a run, and an inspection point that a shorter window cannot absorb.
The tiered quote is the honest form of a lead time because it names the workload behind the date. A shop that quotes one flat lead time for everything has not counted the steps; one that quotes a tier with the routing explained has. The DFM review at quoting is where the routing is counted and the tier is set, which is why the review comes before the date. When you ask what moves the part to a faster tier, the answer usually points to a step the drawing does not need, and removing it is the honest way to shorten the schedule.
Why should the capacity check come before the date?
A lead-time promise is only as real as the capacity behind it, which is why the capacity check belongs at the start of a machining project, not after the date has been missed. Ask for three things in writing: the machine list by type and count, a recent inspection report on a part similar to yours, and the material verification method. The machine list shows whether the shop has the axis classes and processes your geometry needs; the inspection report shows whether its quality room can measure what the drawing demands; the material verification shows whether the stock story is real.
The capacity check also answers the question that decides delivery: what else is on the floor. A shop with machine depth can schedule your part without waiting on a single spindle, and a rush or a ramp from another customer does not displace your date the way it would on a one-machine floor. When a supplier names its machines and its inspection equipment and welcomes a visit to reconcile the list against the floor, the capacity is real; when it hesitates or deflects, the date it quotes is a hope wearing a schedule. Verify capacity before you commit a schedule to it.
Machine depth is not the same thing as available capacity, and a buyer should separate the two. A shop may own many machines and still be fully committed to other programs; the honest question is what the schedule looks like this month, not what the capability sheet shows. Ask how long the queue is for the machine class your part needs, how the shop sequences rush work without displacing committed dates, and whether the inspection room can measure your part's critical features inside the same delivery window. Those three answers — machine queue, sequencing policy, and metrology capacity — are the actual delivery forecast, and a supplier that gives them in numbers is quoting a real schedule. One that answers only with a machine count is showing you inventory rather than capacity, and that distinction is exactly what decides whether your date holds.
What puts a part in each tier, and which step owns the schedule?
The tier is set by the process steps, and the step count is the honest driver of the date. A simple part runs in a handful of steps; a complex part can reach many operations, adding cross-features, secondary processes, and the inspections between them. The table below maps the common characteristics to the tier they usually land in.
| Part characteristic | Typical tier | What owns the schedule |
|---|---|---|
| Simple part, standard material, no finish | About 3 days | A short routing with few operations |
| Moderate features, routine inspection | About 7 days | More operations and setups |
| Many operations, thin walls, tight callouts | Toward 30 days | Sequencing and longer machine time |
| Surface finishing or heat treatment in the route | 30-day tier | Processor queues and post-treatment work |
| Special-order or exotic material | 30 days or longer | Material procurement ahead of machining |
Complexity decides the tier; quantity is a second-order effect. A single complex part and a production run of the same geometry share a tier, because the schedule is set by the work rather than the count, and volume adds machine time that a shop with depth schedules in blocks. Quantity only starts to move the date beyond a production threshold, where the run occupies a machine for a measurable stretch and has to be planned as a block. That is why repeat volume is quoted against its own schedule rather than against the prototype tier, and why the quantity on the RFQ matters as much as the drawing. State the real volume when you ask for the date, and the tier you receive will describe the order you actually intend to place.
For most parts the machining itself is not the bottleneck — the steps around it are. Material procurement owns the schedule when the stock is special-order. Finishing owns it when the process runs at a specialist with its own queue. Final inspection owns it on complex parts, where the metrology is real time. Ask which step owns your date, and you will know where the schedule can be shortened and where it cannot.
How does material availability sit in the schedule?
Machining cannot start until the stock is on the floor, which puts material availability at the front of any schedule. Standard alloys sit in stock at most shops, and a part in one of those can start the moment the program is approved. A special-order alloy, a non-standard size, or a material that must arrive with a certificate moves procurement onto the critical path, and the machining tier alone no longer describes the schedule — the procurement time has to be added in front of it.
The buyer's control is to ask at quoting whether the material is in hand and, if not, what the procurement time is. On a functional part, also ask whether the production material is required for this order at all — a geometry validation can often run in a standard stock grade, moving the order off the procurement path while the material-specific validation waits for the production-grade first article. Material decisions are schedule decisions, and making them at quoting instead of after the order is how machining dates stop slipping.
Freight and customs belong in the schedule for a shop that serves export buyers, because the tier is a machining number and the delivery is a door-to-door number. International courier transit for a small order typically adds days to the tier, sea freight for volume adds weeks, and customs clearance and the buyer's own receiving inspection sit between the courier's delivery and the parts being usable. Confirm the shipping method, the transit time, and the Incoterm when the order is placed, and add the freight to the machining tier when you plan the delivery date. A program that plans the tier plus the freight plus the receiving check is one whose launch date holds; one that plans to the machining date alone discovers the gap when the parts arrive after the line needed them.
What do drawing changes and quality gates do to the schedule?
A machining schedule is built around a frozen drawing, and every change resets part of the clock. A revision that moves a feature means a program edit, a new first article, and usually a fresh inspection; at production volumes it also means a new setup for the affected operations. Batch your changes into one release rather than emailing them one at a time, and ask what a revision does to the date before you send it. A change that moves a hole may cost a day; a change to a finished surface may move the part down a tier.
Quality gates sit inside the schedule and are worth planning around. The first-article inspection on a new part, the CMM run on the key characteristics, and the material certificate check are the steps that keep a fast part from becoming a rejected one. Ask when the first article will be measured and reported, that date is the real proof point of the schedule. A shop that schedules the quality gates as part of the routing is running a schedule you can trust; one that treats inspection as spare time is promising dates it cannot hold.
How do you compress a machining lead time without hurting quality?
Compression comes from removing steps and planning the ones that remain. Run the DFM review with the schedule in view — every operation that a small design change eliminates is schedule recovered, and the features that fight the process are the ones the review should flag. Approve the material and the finish at quoting so no decision waits on a later email, confirm the documentation list so the report is produced to your template on the first pass, and tell the shop which date matters so it can plan the capacity and the sequence around it.
Then use the machine depth deliberately. A part that can run on more than one machine class should be scheduled across the floor rather than queued on one spindle, and a production ramp should be planned in steps the capacity absorbs rather than a jump it cannot. When a date is truly critical, say so early and ask what the fastest honest route is, not a rush on the current process, but a routing that reaches the same result in fewer steps. The compression that happens at quoting is the only kind that is free, and the capacity that backs the date is the only kind that holds.
One schedule decision compounds across a program: the release cadence. A program that orders the prototype, then a validation batch, then production in three separate releases pays three setups and three lead-time tiers; one that sequences the releases so the validation batch follows the approved first article and production follows the validated report pays each setup once and lets each stage's output feed the next decision. On repeat production, a release covering several weeks of consumption runs once and carries one lead time, while the same volume split into small releases restarts the setup and the tier on every batch. The cadence is where lead time and cost meet, and planning it deliberately is what turns a series of orders into a program with dates that hold.
How do you plan a program across prototype, repeat, and production?
Lead time has to be planned at every stage of the program. Prototype at MOQ 1 while the design is unproven, because a design error costs a single part and the first article sets the process. Move to a validation batch once the design is stable, and use its report to lock the routing and the documentation format. Then schedule production from the proven numbers, sharing the forecast so the shop can plan machines and material around the program rather than fitting it into gaps.
Plan backward from the need date at every stage: the machining tier, plus freight, plus receiving inspection, plus the buffer. Work the calendar back from the assembly or launch date and the placement date appears, and it exposes the schedule discipline most programs learn the hard way, which is that the prototype was never the bottleneck; the decisions around it were. The services page on this site explains how machining, finishing, and inspection are combined into a route, and the capacity FAQ covers the machine list, the inspection evidence, and the material verification behind the dates.
Frequently Asked Questions
What is a realistic lead time from a CNC machining shop?
Roughly 3, 7, or 30 days, set by part complexity and process steps. Simple parts run about 3 days, standard parts about 7, and complex parts about 30. The tier follows the routing, not the order size, so a single flat date for every part is usually a guess.
Why should I ask for a capacity check before the date?
Because a lead-time promise is only as real as the capacity behind it. Ask for the machine list, a recent inspection report on a similar part, and the material verification method before trusting a date. A shop with real capacity answers in evidence.
Which step usually owns my machining date?
Ask which operation is on the critical path. It is usually material procurement when the stock is special-order, a finishing or heat-treatment step with its own queue, or final inspection on a complex part. The machining itself is rarely the bottleneck on a deep floor.
How do I get a shorter lead time without hurting quality?
Compress the schedule by removing steps, not rushing them. A design that machines in fewer operations ships faster; material in stock starts sooner. Tell the shop which date matters and approve the decisions at quoting so none waits on a later email.
Does a bigger order take longer than a small one?
Up to a threshold, no — the tier is set by the process steps, and volume adds machine time a capable shop schedules in blocks. Beyond that threshold the quantity does move the date, which is why repeat volume is planned on its own schedule.
How much buffer should I add beyond the quoted tier?
Add the freight transit to the machining tier for the delivery date, then a short buffer for the assumptions that can slip. The tier is machining days, not door-to-door days. A buffer absorbs the first slip without turning it into a crisis.
What should I send to get a fast, accurate date?
The complete package in one message — the drawing at a final revision, the material with its condition, the tolerance and finish callouts, the quantity, and the target date. The fewer questions the shop must ask, the sooner the tier is set. Completeness is the cheapest expedite.
Planning an order and want a date with the schedule explained?
Email [email protected] or call +86 13126536955 and ask for the tier, the routing behind it, and the capacity evidence that backs it.